Hey there, fellow fabricators, welders, and anyone who’s ever stood in a workshop surrounded by humming tools, metal shavings, and the urgent need to get a job done right. If you’ve worked with CUT welding machines for any length of time, you’ve probably heard the phrase “heat input” thrown around—sometimes like it’s the magic number that makes or breaks a part, other times like just another jargon term to muddle through. When I started out in the welding industry, back when I was just a kid sweeping up floor shavings and helping my dad’s team of welders prep steel for custom railings, I had no clue how critical heat input really was. I thought more heat meant faster work, right? Turns out, that’s like pouring gasoline on a small campfire to keep it going—you get a big, messy blaze that burns through everything before you can adjust. These days, I’m a supplier of CUT welding machines, and I spend almost every day talking to workshop owners, master welders, and even folks who are new to the game and just trying to figure out why their last project turned out warped, brittle, or full of cracks. So today, I want to break down exactly what the heat input of a CUT welding machine is, why it matters more than you think, and how getting it right can save you time, money, and a whole lot of headaches on every job. CUT Welding Machine

First off, let’s get the basics straight: what even is a CUT welding machine? For those who might be a little rusty (pun very intended), CUT stands for Carbon Underwater Cutting and Welding—though these days, the term is used more broadly to describe machines that combine precision cutting with high-quality arc welding, perfect for everything from shipbuilding and pipeline repairs to custom metal fabrication and auto body work. Unlike older welding machines that only did one job, CUT machines are built to switch between cutting and welding seamlessly, which is why they’re so popular in industries where versatility is non-negotiable. But here’s the thing that trips most people up: whether you’re cutting a ½-inch steel plate or welding two pipes together, the core of the machine’s performance hinges on that one term we’re talking about: heat input.
Let’s define heat input in plain, workshop-friendly language, no fancy equations that’ll make you reach for your coffee. At its simplest, heat input is the total amount of thermal energy that a welding arc delivers to the workpiece per unit of length of the weld. It’s not just about how hot the arc is (though that’s part of it)—it’s a combination of three main factors: the welding current (that’s the flow of electricity from the machine to the electrode), the voltage of that arc, and the speed at which you move the torch along the weld joint. Think of it like pouring water into a bucket: if you turn the faucet on high, move fast, you’ll get a shallow layer. If you turn it on low and move slow, you’ll fill the bucket deeper, but it’ll take longer. Heat input works exactly the same way with your welding arc. If you’ve ever had a weld that looked good on the surface but cracked a week later, or a workpiece that warped so bad it didn’t fit the design, chances are heat input was off.
Now, why does this matter so much for CUT welding machines specifically? Let’s take a real example from a job last month that a customer of mine brought to me. It was a small fabrication shop in the Midwest, making custom steel frames for agricultural equipment—think big, heavy frames that hold combine harvesters together. They were using a CUT machine to weld ⅜-inch mild steel, and their welder, Jake, was cranking up the current to 250 amps, running at 28 volts, and moving the torch at about 8 inches per minute. The welds looked thick and strong when they finished, but after a couple of weeks on the farm, several of the frames cracked right at the weld joints. Jake called me frustrated, saying the machine must be faulty. When we walked through the numbers, we calculated his heat input was around 45 kilojoules per inch. For ⅜-inch mild steel, that’s way too high. What was happening? The extra heat was making the weld metal too brittle, and it was also warping the frame—because when you heat a piece of steel unevenly, it expands, and when it cools, it contracts unevenly, creating stress. The fix? Drop the current to 180 amps, keep the voltage around 26, and speed up the torch to 15 inches per minute. That brought the heat input down to 22 kilojoules per inch, and those frames have been going out without a single crack in six weeks. That’s the real impact of getting heat input right—it’s not just a number on a spec sheet, it’s the difference between a job that lasts and a job that comes back to bite you.
Let’s get into the science a little, because understanding the “why” helps you adjust when things go wrong. The formula for heat input (HI) is actually pretty straightforward: HI = (Current × Voltage × 60) / (Travel Speed). The 60 is there to convert seconds to minutes, since travel speed is usually measured in inches per minute or millimeters per minute. So if you’re running 200 amps, 25 volts, and moving at 10 inches per minute, your heat input is (200 × 25 × 60) / 10 = 30,000 joules per inch, or 30 kilojoules per inch. Now, different materials and different thicknesses have ideal heat input ranges for a reason. For example, if you’re welding thin aluminum for a boat hull, you’ll need a much lower heat input—too much and you’ll burn through the metal, creating holes that are a nightmare to fix. For thick stainless steel used in chemical tanks, you might need a slightly higher heat input, but not so high that you cause corrosion or weaken the base metal’s structural integrity. CUT welding machines are built to adjust these three factors (current, voltage, travel speed) precisely, which is why they’re better than older, less precise machines for getting heat input right. But here’s a common mistake I see: a lot of welders just crank up the current when they need a deeper penetration, not realizing that faster travel speed can give the same penetration without the extra heat. That’s the beauty of modern CUT machines—many have digital displays that show real-time current and voltage, so you can adjust on the fly, instead of guessing like we did back in the old days.
Another thing that’s often overlooked when talking about heat input with CUT machines is the type of welding process you’re using. Most CUT machines are compatible with MIG (Metal Inert Gas), TIG (Tungsten Inert Gas), and sometimes even stick welding, though MIG is the most common for high-volume jobs. Each process has its own heat input characteristics. For example, MIG welding has a “spray transfer” mode that uses higher current and lower voltage, which gives a deeper penetration with a slightly lower heat input than stick welding for the same amperage. TIG welding, on the other hand, uses a thinner arc, so it’s better for thin materials where you need precise, controlled heat—perfect for custom work where aesthetics matter as much as strength. When a customer comes to me asking for a CUT machine, I always ask what they’re welding, what thickness, and what their end goal is, because that changes the ideal heat input they need. A shipyard welding 1-inch steel plates for a new vessel has totally different heat input needs than a custom furniture maker welding 16-gauge steel for a table leg.
Let’s talk about the costs that come with getting heat input wrong, because that’s what makes this a conversation that workshop owners can’t ignore. I once worked with a guy who owned a small fabrication shop in Texas, and he was losing about $12,000 a month in rework because of bad welds. When we checked his process, he was running way too high heat input on his ¼-inch carbon steel parts, leading to warped pieces that he had to grind down, re-weld, or even scrap entirely. By adjusting his heat input to the ideal range, he cut his rework costs by 70% in the first two months. That’s not just a nice number—it’s profit going back into his business, to buy new tools, hire more help, or raise his margins on jobs. On the flip side, too low heat input is also a problem. If your heat input is too low, you’ll get a weld that doesn’t fuse properly to the base metal, leading to weak joints that can fail under pressure. I’ve seen pipelines leak because of under-heat welds, and that’s not just a workshop mistake—it’s a safety hazard that can cost lives, not just money.
Now, as a CUT welding machine supplier, I’m always asked: which of my machines is best for controlling heat input? The short answer is, any modern CUT machine with digital control and real-time process monitoring is going to give you the precision you need, but there are a few key features to look for. First, a machine that lets you set and lock in your ideal current and voltage, so you don’t accidentally crank it up mid-job. Second, a display that shows you real-time travel speed—either with a built-in sensor or by letting you input it manually, so you can calculate your heat input on the fly. Third, compatibility with multiple welding processes, so you can switch between MIG for heavy work and TIG for delicate jobs without changing machines. I always tell my customers that the best CUT machine isn’t the one with the highest amperage—it’s the one that lets you control the heat input accurately for your specific materials and jobs. For example, if you’re working on a lot of thin aluminum or stainless steel, a CUT machine with a pulsed MIG function is a game-changer. Pulsed MIG alternates between high and low current, so you get deep penetration when you need it, but less overall heat input—perfect for preventing warping and burn-through.
Let’s wrap this up with some practical tips that you can use on your next welding job, no matter what machine you’re using. First, look up the ideal heat input range for your material and thickness. There are standard tables for most common metals (mild steel, stainless steel, aluminum) that will tell you the recommended kilojoules per inch. Don’t guess—use these as your starting point. Second, track your current, voltage, and travel speed for every weld. If you’re using a digital CUT machine, this is easy—most store this data for you, so you can go back and adjust if a weld fails. Third, test on scrap metal first. I can’t stress this enough. Weld a few scrap pieces of the same material and thickness as your actual job, adjust your heat input until you get a weld that has good penetration, no brittleness, and no warping, then use those settings for the real job. Fourth, if you’re dealing with thick materials that need multiple weld passes, adjust the heat input for each pass. The root pass (the first one that fuses the two base metals together) needs a little more heat to get good penetration, but the fill and cap passes can use lower heat to avoid overworking the metal.
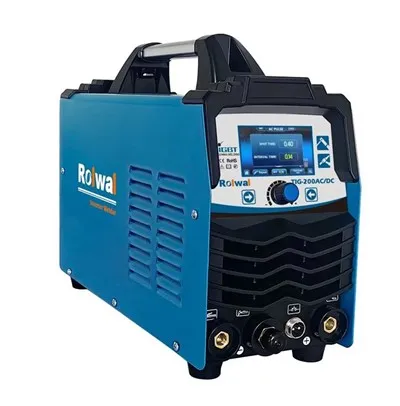
At the end of the day, heat input isn’t just a technical term—it’s the core of a good weld. Whether you’re a master welder with 30 years of experience or a new hire who just got their welding certification, paying attention to heat input will make your work stronger, more consistent, and less costly. As someone who’s spent years in this industry, from sweeping floors to talking to customers about their equipment needs, I’ve seen firsthand how a little knowledge about heat input can turn a struggling workshop into a profitable one. If you’re ready to upgrade your CUT welding machine to get better control over heat input, or you just have more questions about how to apply these concepts to your specific jobs, I’m here to help. We work with workshops of all sizes, from small custom fabricators to large industrial operations, and we’ll help you find the right CUT machine that fits your needs and budget, so you can stop stressing about weld failures and start producing work you can be proud of. Don’t wait until your next job has a crack or a warp—get in touch to learn more about how our CUT welding machines can help you master heat input and take your work to the next level.
MIG Welding Machine References
Lancaster, J. F. (1986). Metallurgy, principles, and procedures of welding. American Welding Society.
American Welding Society. (2018). Welding process and related operations terminology (AWS A3.0). American Welding Society.
Messler, R. W. (2004). Joining of materials: Principles, techniques, and processes. Elsevier.
Lewei Pumps Industry Co., Ltd.
Lewei Pumps Industry Co., Ltd. is one of the most professional cut welding machine manufacturers and suppliers in China, featured by quality products and low price. Please rest assured to buy bulk discount cut welding machine for sale here and get free sample from our factory. Also, customized service is available.
Address: Shanshi Industrial Zone, Daxi Town, Wenling City, Zhejiang Province, China
E-mail: info@rolwal.com
WebSite: https://www.rolwalpumpweld.com/
